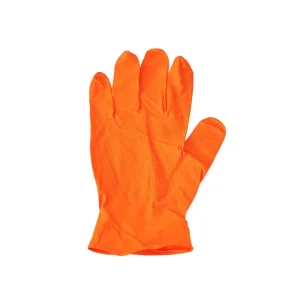
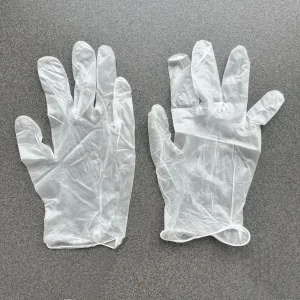
Dongguan Puppelio Glove Co., Ltd. stands globally recognized as a premier manufacturer of disposable sanitary protective gloves, maintaining an uncompromising dedication to professional safety since 1992. With over three decades of engineering excellence, Puppelio serves as a trusted international exporter supplying high-performance hand protection to medical, industrial, pharmaceutical, and laboratory sectors worldwide, including specialized trade channels serving regions like Annaba.
Annaba, a critical coastal industrial hub in Algeria, thrives on heavy manufacturing, steel production, chemical processing, and advanced scientific research. Ensuring worker safety and sample integrity in these rigorous environments requires high-grade barrier solutions. Puppelio bridges the gap between global manufacturing scale and local Annaba industrial compliance, providing customized protective solutions engineered for extreme heat, chemical corrosives, and cleanroom precision.
Send Inquiry Now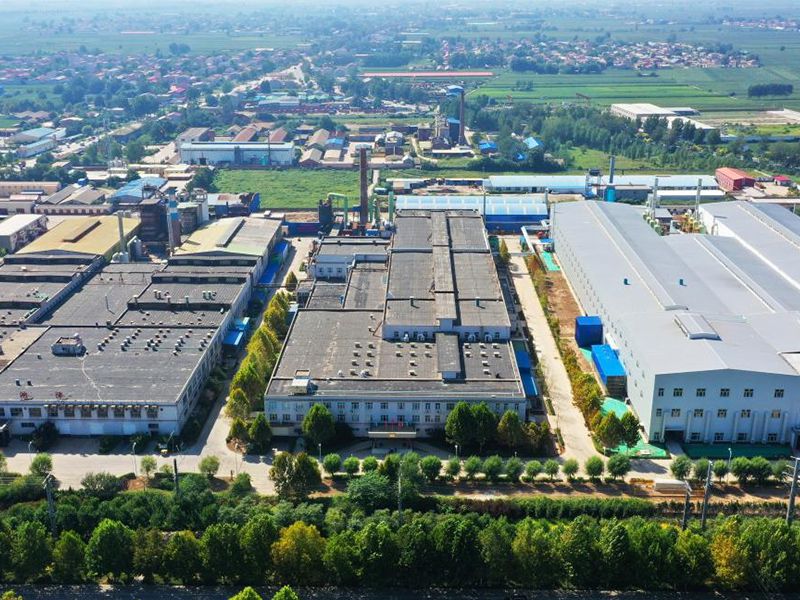
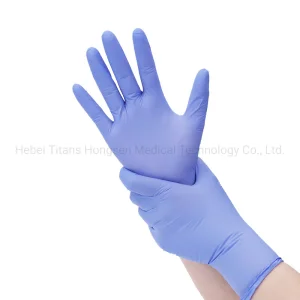
Operating 10 advanced production bases strategically located across Hebei, Shanxi, and Yunnan provinces in China, Puppelio commands 219 state-of-the-art production lines. This massive infrastructure cements our position among the world's most capable industrial glove manufacturers.
We specialize in six primary categories comprising over 120 specialized product variations. Our catalog covers vinyl gloves, nitrile gloves, vinyl/nitrile composite blend gloves, cleanroom specialized gloves, NBR latex gloves, and diverse PE barrier products. Each article undergoes stringent physical, chemical, and biological testing to guarantee absolute compliance with international safety protocols (ASTM, EN374, ISO 9001).
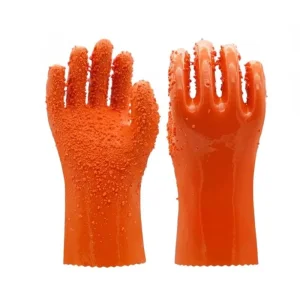
Annaba is renowned as Algeria's industrial powerhouse, notably hosting major metallurgical operations like the El Hadjar steel complex. Technicians, maintenance crews, and metalworkers require heavy-duty chemical protection and mechanical resistance gloves to prevent injuries from sharp edges, lubricants, and caustic solutions.
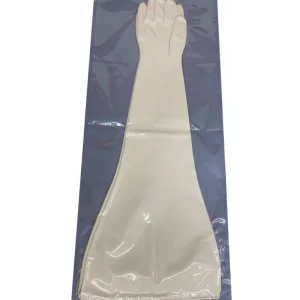
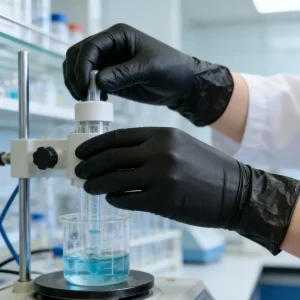
With regional petroleum refining and chemical manufacturing facilities, laboratory technicians in Annaba demand specialized barrier protection. EPDM, heavy-duty nitrile, and specialized chemical-resistant gloves protect researchers against hazardous solvents, acids, and volatile reagents during testing and quality assurance.
Healthcare expansion across Annaba drives continuous demand for powder-free nitrile and latex examination gloves. Sterility, tactile sensitivity, and allergen-free formulations are paramount for pharmaceutical compounding, clinical diagnosis, and hospital sanitation protocols.
Dongguan Puppelio combines cutting-edge R&D with flexible manufacturing capabilities. We understand that global B2B procurement managers and distributors in markets like Annaba require tailored solutions. Therefore, we offer comprehensive OEM and ODM customization services, empowering clients to specify exact dimensions, barrier thicknesses, surface textures (such as diamond grip or micro-textured fingertips), custom packaging configurations, and private-label branding.
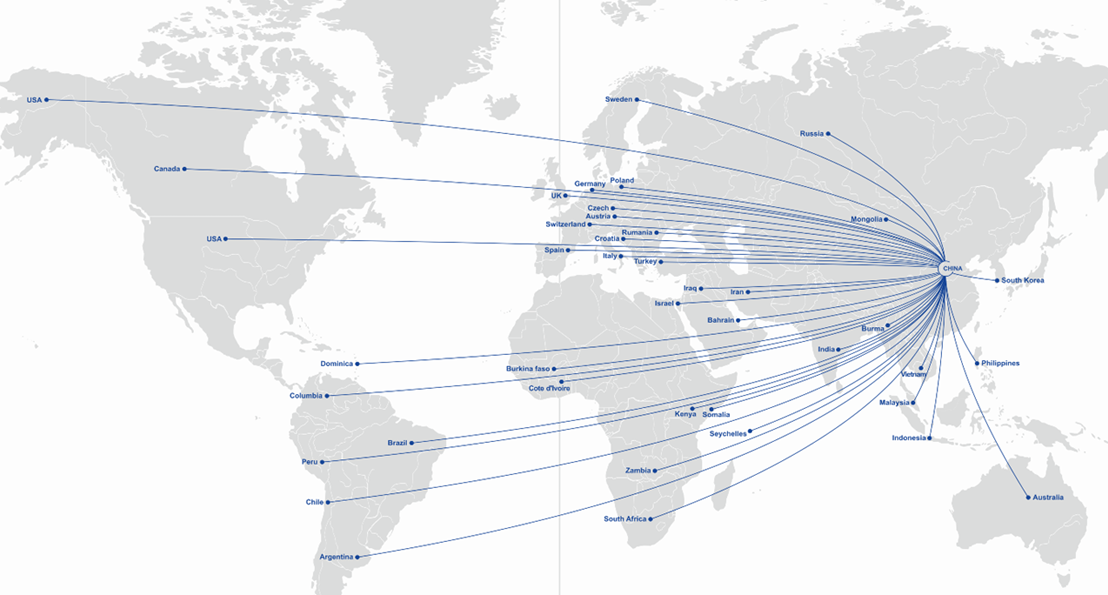
Our expansive global distribution network and dedicated multilingual after-sales support team ensure seamless logistics execution, timely port deliveries, and responsive customer service. Whether supplying a network of regional medical distributors or equipping industrial conglomerates in North Africa, Puppelio maintains uncompromised standards of reliability.
The global protective glove market is undergoing rapid transformation driven by stringent workplace safety regulations, technological breakthroughs in polymer science, and heightened environmental awareness. Key trends shaping the future of laboratory and industrial glove manufacturing include:
As a market leader, Puppelio heavily reinvests in sustainable R&D, ensuring our partners in Annaba and across the globe receive cutting-edge, future-proof protective gear.
For heavy chemical handling, EPDM gloves and ultra-thick chemical-resistant nitrile gloves are recommended due to their superior resistance against acids, bases, and organic solvents. For light laboratory work, standard powder-free nitrile or PVC gloves offer optimal dexterity and comfort.
Yes, we provide extensive OEM/ODM solutions. Clients can customize glove thickness, color, surface texture, box packaging design, and embossed brand logos to meet specific regional regulatory standards and market preferences.
We operate 219 advanced production lines backed by rigorous ISO 9001 quality management systems. Every batch undergoes automated leak testing, physical tensile strength verification, and chemical residue analysis prior to shipment.
Explore our comprehensive selection of specialized barrier gloves designed for high-performance safety across diverse industries.
 Puppelio Glove