Explore our elite portfolio of certified sterile surgical gloves, high-grade medical examination barriers, and specialized industrial hand protection manufactured to stringent international standards.
Decades of manufacturing precision, unparalleled infrastructure, and an unwavering commitment to global health safety standards.
Navigating the shifting paradigms of sterile surgical glove manufacturing, stringent hospital standards, and large-scale international supply chain requirements.
The global healthcare sector demands heightened levels of sterile barrier protection. As surgical procedures increase worldwide, the focus has shifted toward hypoallergenic, ultra-sensitive, and fatigue-reducing surgical gloves. Modern hospitals and surgical centers require products that eliminate chemical accelerators, preventing Type IV hypersensitivity while maintaining high tensile strength and puncture resistance.
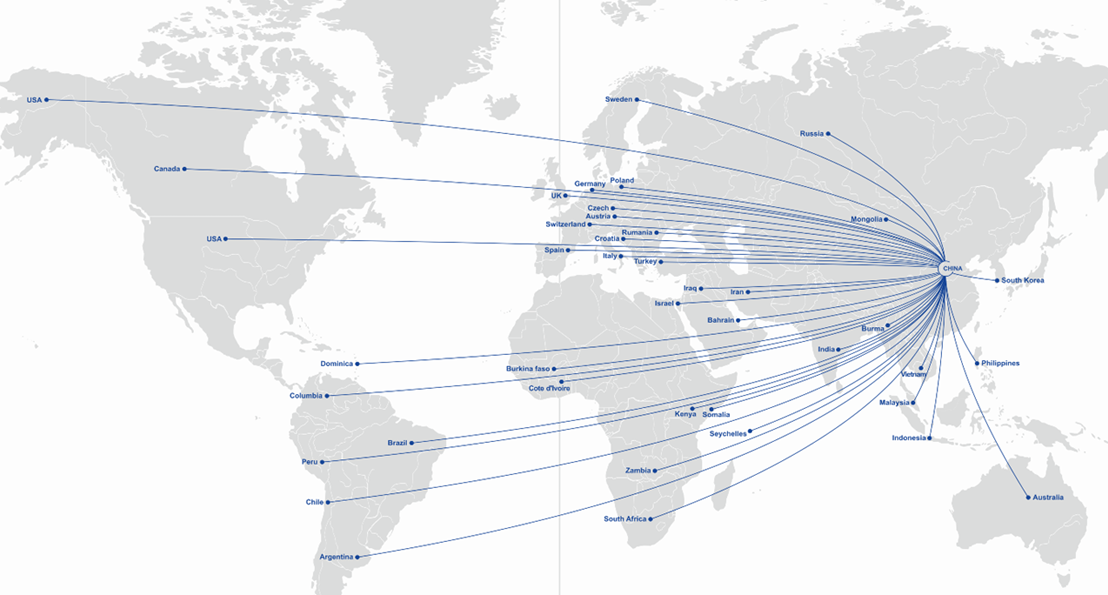
Global procurement officers from group purchasing organizations (GPOs), ministries of health, and industrial distributors prioritize supply chain resilience, scaling capability, and uncompromised regulatory compliance. Buyers seek direct-manufacturer partnerships in China that offer guaranteed capacity, transparent batch traceability, and rapid logistical turnaround to safeguard medical operations against unforeseen supply disruptions.
Comprehensive frameworks designed to meet exacting international standards across FDA, CE, ISO, and localized clinical requirements.
We offer comprehensive customization packages ranging from custom glove formulation, thickness optimization, and specialized surface chlorination or polymer coating, to bespoke sterile packaging designs and private label carton printing.
Our manufacturing facilities operate under strict ISO 13485, CE MDR, and FDA QSR guidelines. Every batch of sterile surgical and examination gloves undergoes rigorous pinhole testing, tensile strength trials, and sterility validation.
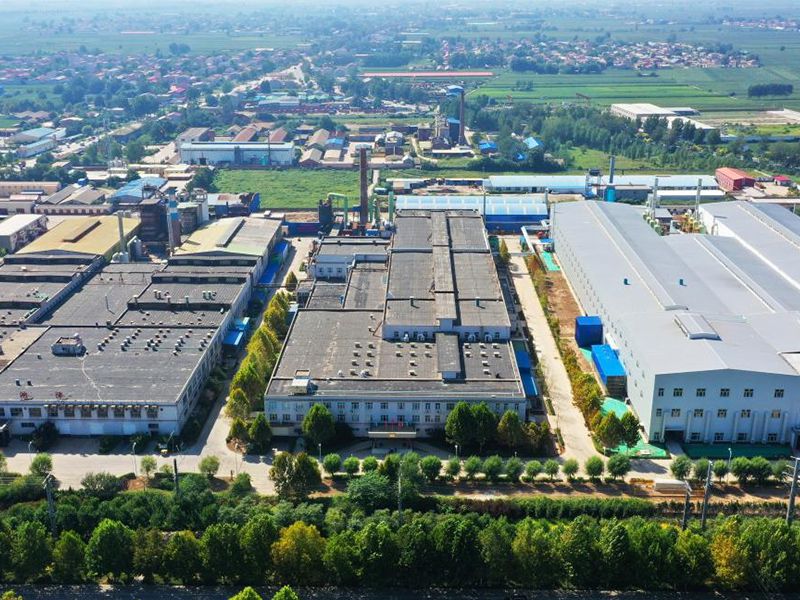
Addressing modern ecological mandates, Puppelio pioneers biodegradable nitrile formulations and energy-efficient closed-loop water recycling systems across our 10 production bases, minimizing carbon footprints without compromising barrier safety.
Discover our wider ecosystem of high-performance industrial safety, cleanroom, food-safe, and eco-friendly disposable hand protection.
Pioneering the next generation of smart manufacturing, automated defect detection, and advanced biomedical polymer engineering.
Integrating high-speed machine vision and artificial intelligence across all 219 production lines to detect microscopic pinholes and inconsistencies in real-time, ensuring zero-defect delivery for critical surgical applications.
Ongoing collaboration with premier materials science laboratories to develop ultra-thin, high-tactile sensitivity surgical gloves that mimic bare-hand dexterity while exceeding barrier protection standards.
Expanding strategic warehousing and logistical hubs across key international markets to reduce lead times, optimize inventory management, and provide localized support for global healthcare distributors.
Expert answers regarding our manufacturing capabilities, quality certifications, and global procurement procedures.
 Puppelio Glove